
Industrial Automation
Quality Inspection
& Defect Detection
AI-powered inspection systems tied to production decisions, evidence, and deployment on Connect Tech Edge hardware
By Kara Price
Senior Marketing & Events Specialist | Content Strategy | Campaign Execution | Connect Tech Inc.
Technical review: Rob Callaghan, Chief Product Officer, Connect Tech Inc.

Key Takeaways
- CTai LABS helps quality and engineering teams turn a defect-detection goal, existing inspection cell, or trained model into a production decision system.
- An engagement can begin with an idea, a defect definition, existing inspection equipment, a small dataset, a trained model, or a line that produces too many false decisions
- Connect Tech hardware with NVIDIA® Jetson™ modules keeps sensitive production imagery and inference close to the process
- NVIDIA TensorRT™ and CUDA® can accelerate classification, detection, segmentation, and anomaly-detection pipelines after task accuracy is protected
- Validation separates correct accepts, correct rejects, false rejects, and missed defects across product variants and operating conditions
- The customer retains its data, model, product, process knowledge, and intellectual property
CTai LABS quality and engineering teams can work can cover image formation, sampling and labeling, classification, detection, segmentation, anomaly detection, confidence handling, part traceability, reject timing, PLC or MES integration, performance optimization, and validation. CTai LABS can start with only the quality outcome and process knowledge, or join at any point to repair a station, reduce false rejects, address missed defects, integrate new hardware, add product variants, or prepare a deployment-ready release.
Quality inspection begins with the cost of a wrong decision
Inspection performance is not described adequately by one accuracy number. A false reject can create scrap, rework, line disruption, and manual-review cost. A missed defect can allow nonconforming material to move downstream or reach a customer. The acceptable operating point depends on defect severity, process capability, downstream containment, inspection coverage, review capacity, and the action the system controls.
CTai LABS translates those business and process consequences into an acceptance matrix. Precision, recall, specificity, false-reject rate, miss rate, localization quality, calibration, and decision latency are selected according to the inspection task. Metrics are reported by product variant, defect class, operating condition, and confidence band so aggregate performance does not hide an important failure mode.
Patrashko and Gurau (2026) reviewed more than 50 studies of machine-learning vision for robotic inspection and found strong technical potential, while also distinguishing controlled-study performance from the conditions of high-volume manufacturing. Shukla et al. (2025) identified dataset composition, anomaly diversity, domain shift, and resource requirements as continuing issues in industrial image anomaly detection. Hoang and Tan (2025) demonstrated that illumination remains a material variable even in current anomaly-detection pipelines. These findings support a practical rule: the production imaging process and the evaluation dataset must be designed together.
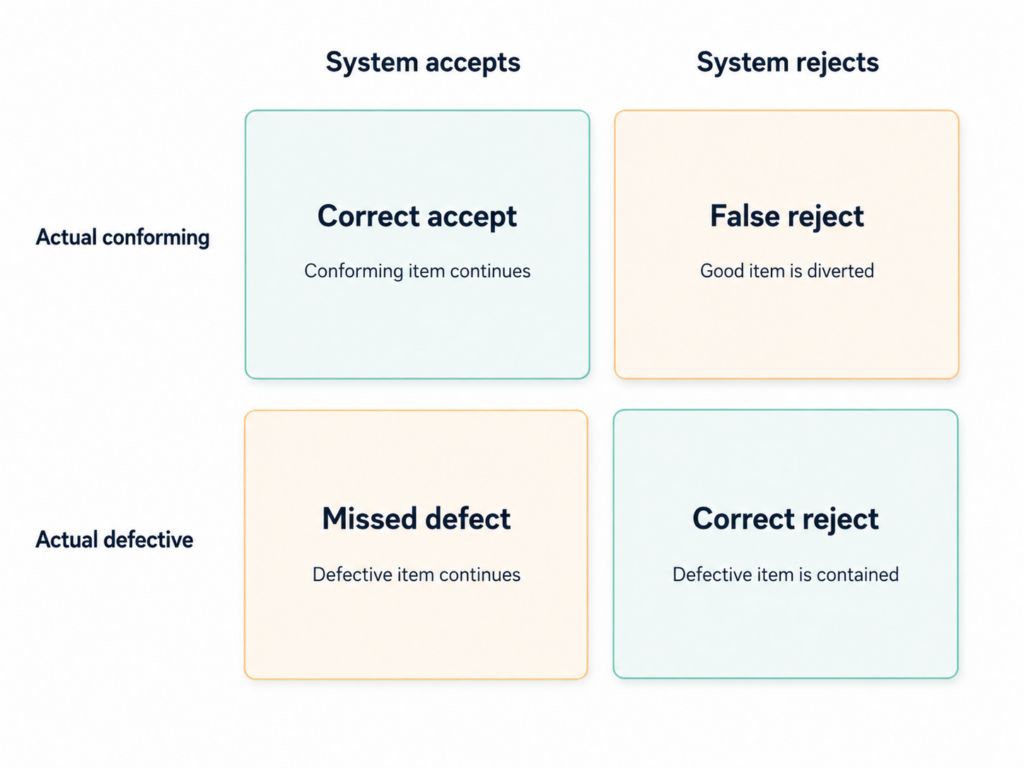
Figure 1. Quality inspection validation must report both false rejects and missed defects because the two errors have different production consequences.
Choose the inspection method from the evidence available
Classification, detection, and segmentation
Classification fits decisions about an entire image or defined crop. Object detection locates instances and supports counts or presence checks. Segmentation provides pixel-level shape or area information for scratches, voids, contamination, material spread, or geometric defects. CTai LABS selects the output that the process needs rather than forcing every problem into one model family.
Anomaly detection for scarce or changing defects
Some processes produce many conforming examples and very few representative defects. Industrial anomaly detection can learn the normal appearance and flag departures for review or containment. Shukla et al. (2025) found that current approaches span reconstruction, embedding, synthetic anomaly, and foundation-model methods, but dataset and deployment limitations remain important. CTai LABS can design a bounded anomaly workflow with known review rules, calibrated thresholds, and a feedback path instead of treating every anomaly score as an automatic reject.
Camera bandwidth and inference are sized separately
A vision station must sustain capture, transport, preprocessing, inference, postprocessing, recording, networking, and operator display at the same time. Peak model frames per second does not prove line-rate operation. CTai LABS measures frame age, drops, queue depth, copies, CPU and GPU contention, memory pressure, storage throughput, network traffic, power, and thermal behavior on the target Connect Tech system under representative production load.
Few-shot and transfer approaches
New products and rare failure modes may not justify a large labeled dataset at the start. Zajec et al. (2024) evaluated few-shot methods for manufacturing defect detection. These approaches can reduce the initial data requirement, but the resulting model still needs evaluation against product variants, nuisance conditions, and production error costs. CTai LABS can compare few-shot, transfer-learning, synthetic-data, and anomaly-detection strategies against the evidence available.
Where defect-detection systems stall
Ground truth is not consistent
If inspectors disagree about the defect boundary, severity, or disposition, the model inherits that ambiguity. CTai LABS can create a defect taxonomy, annotation guide, adjudication process, sample lineage, and golden evaluation set. The work also records uncertain or borderline cases instead of forcing them into labels that appear more certain than the process knowledge supports.
The test split leaks production similarity
Randomly splitting near-duplicate images from the same lot, camera run, or part can overstate generalization. Validation should separate meaningful sources of variation such as time, lot, supplier, machine, tooling state, shift, camera, and product variant. CTai LABS designs the split and acceptance protocol around the way the system will encounter new production data.
The threshold is fixed without production evidence
The model score becomes a production decision only after calibration and threshold selection. CTai LABS can evaluate operating curves, confidence bands, class-specific rules, reject capacity, human-review queues, and escalation behavior. The chosen threshold is versioned with the model and dataset so a future update cannot change the process silently.
A workstation result does not fit the inspection window
High-resolution images, several camera views, multiple models, preprocessing, recording, and interface traffic compete for the same compute and memory. CTai LABS profiles the complete pipeline on Connect Tech hardware, then applies TensorRT precision, batching, concurrency, memory, and data-movement changes only after confirming that the quality decision remains equivalent.
Architecture Through Deployment
- Define the inspected unit, defect taxonomy, severity, disposition, decision window, cost of error, human-review path, and acceptance criteria.
- Assess part presentation, optics, lighting, cameras, triggers, Connect Tech hardware, NVIDIA® Jetson™ module, production interfaces, and data policy.
- Create the sampling, annotation, adjudication, data lineage, train and test split, and change-control plan.
- Select and integrate classification, detection, segmentation, anomaly, few-shot, or combined methods that fit the evidence and production action.
- Optimize the pipeline on the target system and validate task metrics, false decisions, latency, throughput, sustained load, restart, and recovery.
- Deliver the approved model and software release, inspection recipe, threshold record, regression suite, validation evidence, deployment procedure, and handoff.
Connect Tech hardware for quality inspection
The inspection architecture is mapped to camera count and interface, image resolution, model concurrency, decision time, recording, enclosure, and plant integration. Connect Tech camera platforms and Edge systems allow CTai LABS to scale from one compact station to a centralized multi-camera cell.
| Connect Tech platform | Inspection fit | Deployment value |
|---|---|---|
| Hadron-DM or Boson with Jetson Orin™ NX | Distributed inspection points | Compact local inference near the camera with MIPI CSI-2 options, NVMe, and a controlled software baseline across several stations. |
| Lepton with Jetson Orin NX or Jetson Orin™ Nano | Remote-camera inspection | FPD-Link III options for coax-based camera placement where the compute must remain compact and close to the machine. |
| Forge with Jetson AGX Orin™ | Multi-view inspection cells | High-speed networking, NVMe, camera expansion, and compute for concurrent views, models, traceability, and production-system integration. |
| Gauntlet with Jetson Thor™ | Complex multimodal quality analysis | High camera and network bandwidth for several models, high-resolution data, and advanced scene or multimodal reasoning workloads. |
Example Quality Inspection Projects
Surface anomaly inspection with limited defect samples
A manufacturer has thousands of conforming images and only a small set of scratches, dents, stains, and missing-process examples. CTai LABS defines the taxonomy and split, compares anomaly and few-shot approaches, establishes a review band, deploys the selected runtime on Connect Tech hardware, and validates each product and nuisance condition separately.
Multi-view assembly containment
A station must verify components, fasteners, cable routing, and labels from several views before the assembly leaves the cell. CTai LABS integrates synchronized image capture, detection and segmentation models, part traceability, a bounded reject interface, evidence storage, and operator review on Forge with Jetson AGX Orin.

High-consequence conveyor detection
A fast-moving material stream needs detection and response within a measured window. CTai LABS applies the same production architecture demonstrated by the ScrapGuard™ engagement: controlled camera ingest, on-prem inference, event traceability, a defined response interface, and validation against representative material and conveyor conditions. The project scope and acceptance evidence are established for the new process rather than inferred from a different deployment.
Few-shot and transfer approaches
New products and rare failure modes may not justify a large labeled dataset at the start. Zajec et al. (2024) evaluated few-shot methods for manufacturing defect detection. These approaches can reduce the initial data requirement, but the resulting model still needs evaluation against product variants, nuisance conditions, and production error costs. CTai LABS can compare few-shot, transfer-learning, synthetic-data, and anomaly-detection strategies against the evidence available.
What CTai LABS can deliver
- Defect taxonomy, severity and disposition rules, decision-cost matrix, data plan, acceptance metrics, risk register, and validation protocol.
- Imaging, camera, Connect Tech platform, NVIDIA Jetson module, storage, network, power, thermal, enclosure, and production-interface architecture.
- Sampling and annotation guide, adjudication process, dataset lineage, train and test split, golden evaluation set, and change-control procedure.
- Integrated classification, detection, segmentation, anomaly, or few-shot pipeline with calibrated thresholds, review rules, part traceability, and system interfaces.
- Per-class and per-variant performance, false-reject and miss analysis, timing traces, sustained-load results, drift baseline, and known operating limits.
- Versioned model and software release, inspection recipes, regression suite, deployment image, recovery procedure, documentation, and knowledge transfer.
Your Physical ai Integration Partner
CTai LABS connects quality requirements, production data, Connect Tech imaging hardware, Edge ai inference, decision logic, and factory integration in one measurable system. The team can begin with an idea, repair a specific inspection failure, or carry the quality solution from defect definition through deployment while the customer retains its intellectual property.
Book a Demo
Bring your goal. Start with the outcome your quality inspection program must achieve. CTai LABS, a department of Connect Tech, can begin with an early idea, an architecture decision, a working prototype, a difficult integration issue, or a system that needs to become deployment-ready.
What to bring:
- The product, feature, defect, severity, disposition, and production decision the system must support.
- Cycle time, line speed, product variants, lots, process states, review capacity, reject mechanism, and cost of false decisions.
- Cameras, lighting, optics, triggers, Connect Tech or development hardware, NVIDIA Jetson platform, PLC, MES, and data-retention constraints.
- Representative conforming and defective images, labels, adjudicated edge cases, models, logs, and current performance evidence.
- Acceptance metrics, validation population, release milestone, update process, and ownership boundaries.
CTai LABS uses these inputs to identify the highest-risk interfaces first and define the shortest credible path to a working, measurable system.
ABOUT THE AUTHOR
Kara Price
Senior Marketing & Events Specialist | Content Strategy | Campaign Execution |
Connect Tech Inc.
Kara Price is a technology writer covering Edge AI, robotics, and embedded computing for Connect Tech and CTai LABS. Trained in journalism at Humber College with a BA in Communication Studies from Wilfrid Laurier University, she has spent over a decade writing for technical audiences, including four years as a proposal writer in architecture and engineering and ten years publishing product and technical announcements at Connect Tech, an NVIDIA Elite Partner. She is Senior Marketing and Events Specialist at Connect Tech.
 Learn More
Resources and Frequently Asked Questions
Related
Industrial Automation. Explore CTai LABS capabilities for factory-floor machine vision, inspection, predictive maintenance, and rugged Edge ai.
Explore Industrial Automation →Machine Vision AI. Integrate camera pipelines, industrial vision systems, and accelerated ai inference for production environments.
See Machine Vision AI →Predictive Maintenance. Apply sensor data and Edge ai to identify equipment conditions, anomalies, and potential failures earlier.
See Predictive Maintenance →Rugged Edge ai. Engineer Edge ai systems around demanding environmental, power, thermal, connectivity, and deployment requirements.
See Rugged Edge ai →ScrapGuard™. A real-world Edge ai vision deployment for high-risk material detection on a recycling conveyor.
See ScrapGuard™ →Sources
Connect Tech. (n.d.). Forge carrier board for NVIDIA Jetson AGX Orin. Retrieved August 21, 2026, from
https://connecttech.com/product/forge-carrier-for-nvidia-jetson-agx-orin/Connect Tech. (n.d.). Gauntlet carrier board for NVIDIA Jetson Thor. Retrieved August 21, 2026, from
https://connecttech.com/product/gauntlet-carrier-board-for-nvidia-jetson-thor/Connect Tech. (n.d.). NVIDIA Jetson Orin NX products. Retrieved August 21, 2026, from
https://connecttech.com/product-category/form-factors/nvidia-jetson-orin-nx/Hoang, D.-C., & Tan, P. X. (2025). Unsupervised industrial anomaly detection using paired well-lit and low-light images. Journal of Computational Design and Engineering, 12(5), 41–61.
https://doi.org/10.1093/jcde/qwaf043NVIDIA. (2026). TensorRT documentation.
https://docs.nvidia.com/deeplearning/tensorrt/Patrashko, D. Y., & Gurau, V. (2026). Machine learning-powered vision for robotic inspection in manufacturing: A review. Sensors, 26(3), 788.
https://doi.org/10.3390/s26030788Shukla, V., Shukla, A., S. K., S. P., & Shukla, S. (2025). A systematic survey: Role of deep learning-based image anomaly detection in industrial inspection contexts. Frontiers in Robotics and AI, 12, 1554196.
https://doi.org/10.3389/frobt.2025.1554196Zajec, P., Rožanec, J. M., Theodoropoulos, S., Fontul, M., Koehorst, E., Fortuna, B., & Mladenić, D. (2024). Few-shot learning for defect detection in manufacturing. International Journal of Production Research, 62(19), 6979–6998.
https://doi.org/10.1080/00207543.2024.2316279Frequently Asked Questions
What is the difference between defect detection and anomaly detection?
Defect detection learns defined defect classes or regions. Anomaly detection learns normal appearance and flags departures that may not match a known class. The correct method depends on available labels, defect diversity, and the production action.
Can CTai LABS start with only a few defect images?
Yes. CTai LABS can assess anomaly detection, few-shot learning, transfer learning, synthetic-data support, or a staged data-collection plan. The acceptance protocol will reflect the evidence available.
How do you reduce false rejects?
CTai LABS separates image-quality failures, label ambiguity, product variation, model error, calibration, and threshold effects. The operating point is then selected against production costs and human-review capacity.
Can defect detection run fully on-prem?
Yes. Camera ingest, inference, decision logic, traceability, and local evidence handling can run on Connect Tech Edge hardware without sending production imagery to an external service.
Does TensorRT optimization change inspection accuracy?
It can. CTai LABS compares the optimized runtime with the approved model on the same golden dataset and production scenarios before accepting precision or graph changes.
How are new products or suppliers added?
The release can include variant-specific inspection recipes, data lineage, regression sets, approval thresholds, and a controlled model or configuration update process.
Who owns the inspection data and models?
The customer retains its data, process knowledge, models, product design, and intellectual property. Deliverables and third-party licensing boundaries are defined in the engagement.
Ready to Build Smarter?
Let’s create the intelligent Edge AI solution that moves your business forward.